
Body-shop note
Thursday’s audit pulled peel strips from door inners. Nuggets were undersize on the trailing spots of every tip life. The robot TCP sheet was current. Tip dresser hours were not in CMMS.
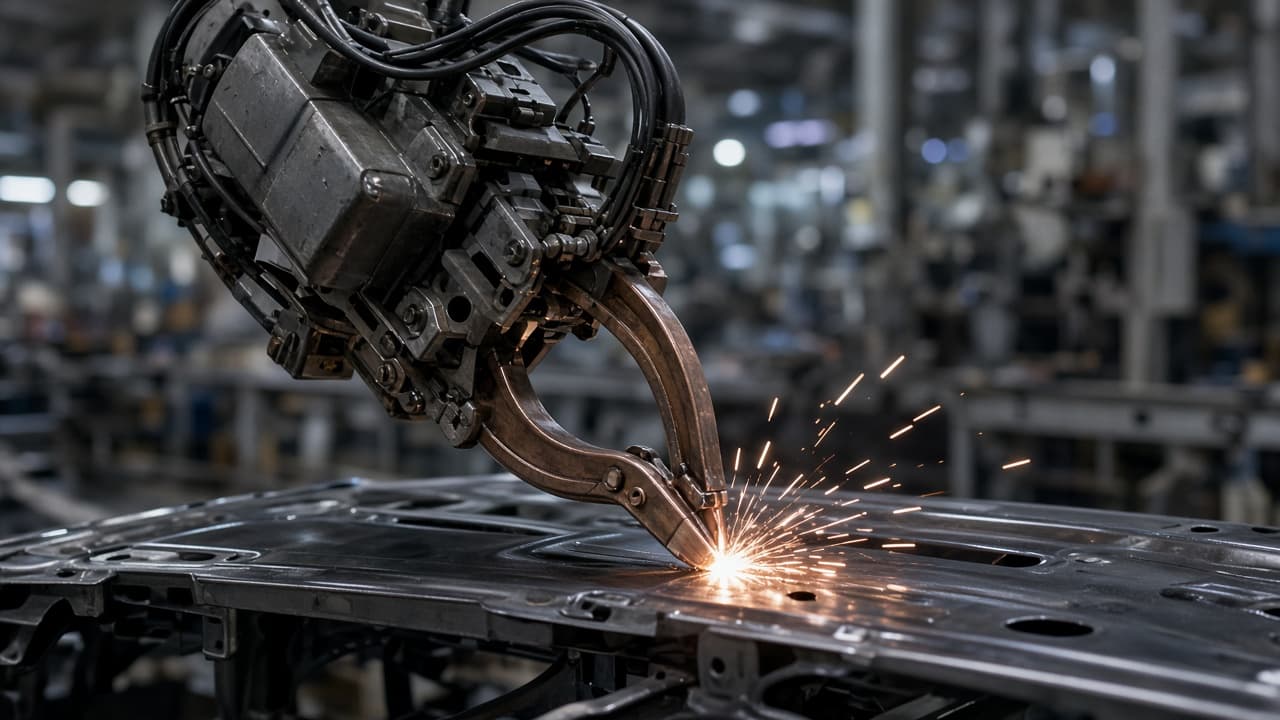
Resistance spot welding on automotive and appliance lines is sold as a gun path and a weld schedule. The arc of current that forms the nugget runs through copper tips. When those tips mushroom or contaminate, contact area grows, current density drops, and the schedule that once made a good nugget makes heat and splash instead.
MIG liner stick-out and adaptive seam tracking own other weld cells. Heat-stake owns plastic. This note owns tip life and tip dressing as the consumable gate on robotic spot weld.
Tip geometry is the process
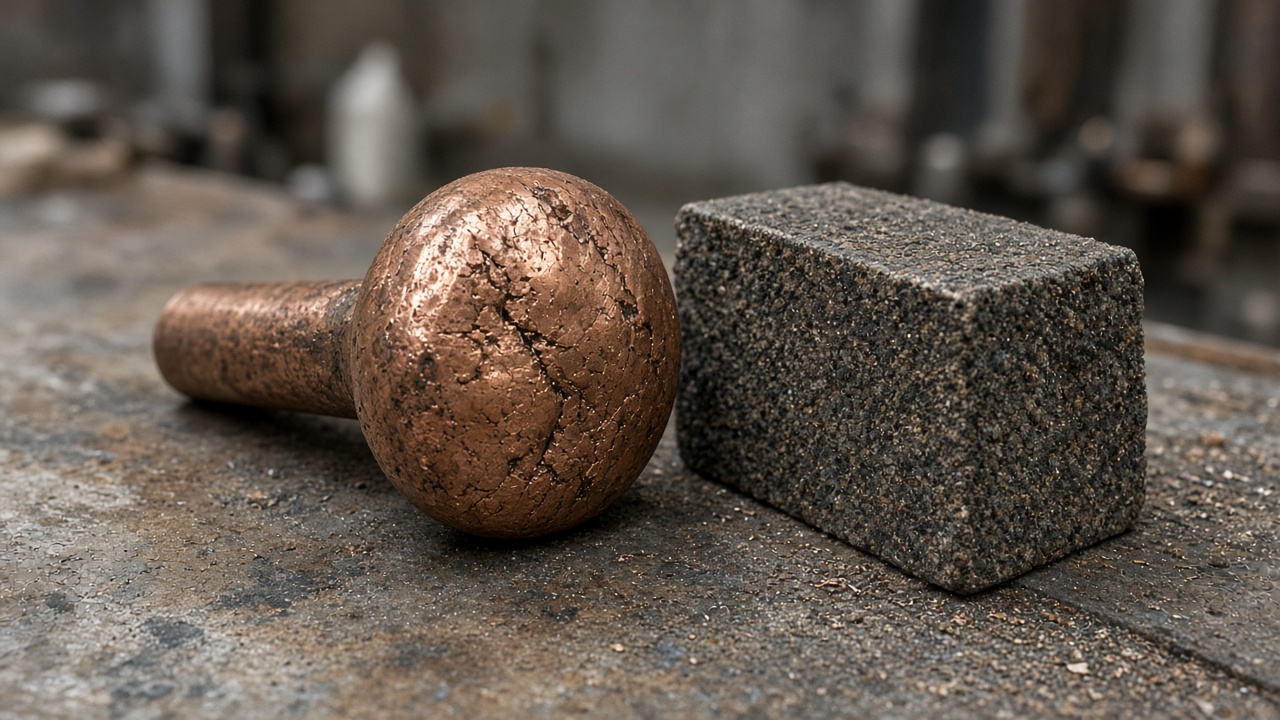
Dressing restores a defined face diameter and contour. Skipping dress cycles to save takt leaves a flat mushroom that still “fires” while peel strength falls. Zinc from coated steel alloys onto the tip; aluminum and adhesives leave other films. Tip change after a hard count—or after a quality trigger—beats waiting for the first customer peel fail.
What to put in the cell story
Log tip ID or gun ID, weld count since dress, dresser stone hours, and expulsion or current-step alarms from the weld controller. Bind tip change to the same MoC as schedule edits for new coatings. If operators can lengthen dress interval from the HMI without a named owner, treat that as a process change—not a convenience.
The robot repeats pose. The tip decides whether that pose still makes a nugget.